.png)
.png)
.png)
How to Size a Containerized Fire Pump Correctly
Sep 04, 2026
Share:
Choosing the correct size for a containerized fire pump is one of the most important decisions when designing a reliable fire protection system. A pump that is undersized may fail to provide the required flow or pressure during an emergency, while an unnecessarily oversized pump can increase equipment, installation, operating, and maintenance costs.
For containerized fire pump systems, sizing involves more than simply selecting a pump based on the required flow rate. The complete system must be evaluated, including fire water demand, required pressure, elevation, pipe friction losses, fittings, equipment losses, water source conditions, pump performance, driver capacity, and applicable fire protection standards.
This guide explains the key factors that engineers, contractors, system integrators, and project owners should consider when sizing a containerized fire pump correctly.
What Is a Containerized Fire Pump?
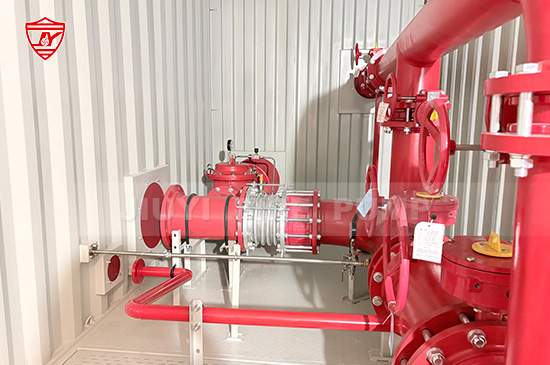
A containerized fire pump is a packaged fire protection system installed inside a specially configured container or enclosure. Depending on the project, the package may include an electric fire pump, diesel engine fire pump, jockey pump, controllers, piping, valves, fuel system, ventilation, exhaust system, monitoring equipment, and other accessories.
Containerized systems are particularly useful when a conventional pump room is difficult or expensive to construct. They can be used for industrial facilities, warehouses, power plants, infrastructure projects, remote sites, construction projects, oil and gas facilities, mining operations, and other locations where a dedicated fire pump building is impractical.
Because many components are integrated into a limited space, correct sizing must consider both hydraulic requirements and the physical requirements of the complete package.
Step 1: Determine the Required Fire Water Flow
The first step in sizing a containerized fire pump is determining the required fire water flow.
The required flow depends on the fire protection system and the hazard being protected. A project may have one or more water-based fire protection systems, including sprinklers, hydrants, hose stations, deluge systems, water spray systems, or other fire suppression equipment.
The design engineer should determine the hydraulic demand of the system according to the applicable project requirements and fire protection standards.
For example, a project may require:
-
500 GPM
-
750 GPM
-
1,000 GPM
-
1,500 GPM
-
2,000 GPM
-
3,000 GPM
The required flow should not be estimated simply from the size of the building. The actual hydraulic design and required simultaneous operating systems should determine the demand.
If several fire protection systems are expected to operate simultaneously, their water demands may need to be combined according to the project design.
The fire pump should then be selected to meet the required flow while providing the necessary pressure at that flow point.
Step 2: Calculate the Required Pump Pressure
Flow rate alone is not enough to select a fire pump.
The pump must also generate sufficient pressure to deliver the required water to the most hydraulically demanding point of the fire protection system.
A useful way to understand the required pump pressure is to consider the major components of total dynamic head.
These commonly include:
Required pressure at the system demand point + elevation head + friction losses + equipment losses + other applicable pressure requirements.
The required pressure at the system demand point comes from the fire protection system design.
Elevation is particularly important for containerized fire pump installations. If the pump is located at ground level while the protected area is significantly higher, additional pressure is required to overcome the elevation difference.
As a general hydraulic relationship, approximately 0.433 psi is required for every foot of water elevation, or approximately 1 bar for every 10.2 meters of water elevation.
For example, if water must be delivered approximately 30 meters higher than the pump, the elevation alone represents roughly 3 bar of pressure requirement.
This pressure must be considered before selecting the pump.
Step 3: Account for Pipe Friction Losses
Water loses pressure as it travels through pipes.
The amount of friction loss depends on factors such as pipe diameter, pipe length, pipe material, flow rate, internal pipe condition, and the configuration of the piping system.
A long discharge pipeline can create significant pressure losses. Selecting a larger pump without understanding the piping system may not be the most appropriate solution. In many cases, reviewing pipe diameter and system configuration can have a major effect on the required pump duty.
Friction losses should also be considered for:
-
Main discharge piping
-
Suction piping
-
Valves
-
Check valves
-
Flow meters
-
Strainers where applicable
-
Elbows
-
Tees
-
Reducers
-
Other fittings and accessories
Each component contributes to the total hydraulic resistance of the system.
For a containerized fire pump package, the internal piping of the container should also be considered. The packaged piping, valves, fittings, and connections can contribute to pressure losses between the pump and the system connection point.
Step 4: Consider Elevation and Water Source Conditions
The location of the water source is another important part of fire pump sizing.
A containerized fire pump may draw water from a storage tank, reservoir, underground tank, open water source, or another approved water supply.
Engineers should determine the relationship between the water level and the pump inlet.
The available suction pressure or suction lift can affect pump selection and configuration. Inadequate suction conditions can cause operational problems even when the pump itself has sufficient rated capacity.
The following information should therefore be evaluated:
-
Minimum water level
-
Maximum water level
-
Pump elevation
-
Tank location
-
Suction pipe size
-
Suction pipe length
-
Suction pipe fittings
-
Available suction pressure
-
Required net positive suction conditions
-
Water temperature and characteristics
Vertical turbine fire pumps, horizontal split-case pumps, end-suction pumps, and other pump configurations have different installation requirements. The water source and site conditions can therefore influence not only pump size but also pump type.
Step 5: Establish the Pump Duty Point
After determining the required flow and pressure, the project team can establish the required pump duty point.
The duty point is generally expressed as:
Flow rate + pressure or head
For example:
1,000 GPM at 120 PSI
or:
1,500 GPM at 100 meters head
This duty point becomes the foundation for selecting the fire pump.
However, the pump should not be selected based only on one theoretical operating point. The complete pump performance curve should be reviewed to understand how the pump behaves across the required operating range.
The pump should provide the required flow and pressure while operating within the applicable performance requirements.
This is especially important for projects where the system demand may vary significantly.
Step 6: Select the Appropriate Pump Type
The required duty point is one of the main factors determining the appropriate fire pump configuration.
Common fire pump types include:
-
End-suction fire pumps
-
Horizontal split-case fire pumps
-
Vertical turbine fire pumps
-
Vertical inline fire pumps
-
Other project-specific configurations
Horizontal split-case pumps are commonly used for larger flow requirements and applications where the installation configuration allows sufficient horizontal space.
End-suction pumps can be suitable for certain smaller or medium-duty applications where the hydraulic conditions and project requirements are appropriate.
Vertical turbine fire pumps are often considered when the water source is below the pump installation level, such as deep tanks, reservoirs, or underground water sources.
The pump type should therefore be selected based on the hydraulic requirements, water source, installation conditions, applicable standards, and project specifications rather than simply choosing the smallest physical pump.
Step 7: Size the Fire Pump Driver Correctly
The driver must be capable of providing sufficient power across the required pump operating range.
Containerized systems commonly use electric motors, diesel engines, or a combination of both.
For an electric fire pump, the motor, controller, power supply, starting characteristics, voltage, frequency, and available electrical capacity must be evaluated.
For a diesel fire pump, the engine must provide sufficient power under the required operating conditions. The package must also accommodate fuel storage, exhaust, ventilation, cooling, batteries, starting equipment, and monitoring systems.
The driver's required power is determined by the pump hydraulic requirements and efficiency.
Choosing a driver that is too small can prevent the pump from achieving its required performance. Choosing a significantly oversized driver may increase package size, cost, and infrastructure requirements.
Step 8: Check the Container Dimensions
Hydraulic sizing is only one part of containerized fire pump design.
The selected equipment must physically fit inside the container while maintaining appropriate access for operation, inspection, maintenance, ventilation, and replacement of components.
A typical package may need space for:
-
Fire pump
-
Electric motor or diesel engine
-
Jockey pump
-
Controllers
-
Piping
-
Valves
-
Fuel tank
-
Batteries
-
Exhaust system
-
Ventilation equipment
-
Cooling equipment
-
Electrical equipment
-
Monitoring devices
-
Maintenance access
The container dimensions should therefore be determined after considering the complete equipment configuration.
A pump may meet the hydraulic requirement but still be unsuitable if the complete package cannot be safely installed and maintained within the available space.
Step 9: Consider Ventilation and Heat Management
Diesel engine fire pumps produce heat and exhaust gases during operation.
A containerized diesel fire pump system therefore requires careful ventilation and exhaust design.
The ventilation system must provide the airflow required for combustion and heat removal while maintaining appropriate operating conditions inside the enclosure.
The design may need to consider:
-
Engine combustion air
-
Radiator airflow
-
Heat generated by the engine
-
Exhaust routing
-
Fresh air intake
-
Hot air discharge
-
Ambient temperature
-
Container insulation
-
Noise considerations
For projects located in hot climates, heat management can become particularly important.
The container should be designed around the actual operating environment rather than relying solely on standard ambient conditions.
Step 10: Consider Fuel Capacity for Diesel Systems
For diesel-powered containerized fire pump systems, fuel capacity should be considered during the design stage.
The required fuel capacity depends on the project requirements, engine characteristics, applicable standards, and expected operating duration.
The fuel tank must also be compatible with the container layout and provide appropriate access for filling, inspection, maintenance, and monitoring.
Fuel system design can affect the overall container dimensions, so it should be considered early rather than added after the pump package has already been designed.
Step 11: Verify Applicable Standards and Certifications
A correctly sized fire pump must also meet the applicable project standards and specifications.
Depending on the project location and application, requirements may involve standards such as NFPA 20 and certification or listing requirements such as UL.
Certification requirements can influence the selection of the pump, motor, diesel engine, controller, valves, and other components.
For projects requiring listed equipment, engineers should verify the certification or listing status of the actual equipment configuration rather than assuming that a similar product automatically meets the requirement.
The complete fire pump package should be reviewed against the project specification before production.
Step 12: Review the Complete Pump Performance Curve
One of the most important steps in fire pump sizing is reviewing the complete performance curve.
The performance curve shows how the pump behaves at different flow rates and pressures.
The engineering team should verify the required operating point against the pump curve and confirm that the selected pump can satisfy the project requirements.
Important points to review may include:
-
Rated flow
-
Rated pressure
-
Shutoff pressure
-
Pressure at various flow conditions
-
Driver power requirements
-
Pump efficiency
-
Operating range
This review helps prevent the common mistake of selecting a pump based only on its nominal flow rating.
For example, a pump described as a 1,000 GPM pump does not automatically mean it will provide the required pressure at 1,000 GPM. The actual pump curve must be checked.
Common Mistakes When Sizing a Containerized Fire Pump
Several mistakes can create problems during project execution.
Selecting the pump based only on flow
A pump may provide the required GPM but fail to generate sufficient pressure at the required operating point.
Ignoring elevation
Projects with significant elevation differences may require substantially more pump pressure.
Underestimating friction losses
Long pipelines and complicated piping systems can produce significant pressure losses.
Choosing the container before the equipment
Selecting a standard container first and attempting to fit the complete system afterward can create access, ventilation, maintenance, and layout problems.
Ignoring ambient conditions
High temperatures, cold climates, dust, humidity, and other environmental conditions can affect equipment selection and container design.
Selecting an inappropriate pump type
The water source and suction conditions should be evaluated before choosing between horizontal, vertical, end-suction, split-case, and other configurations.
Failing to verify certification requirements
A project requiring listed or certified equipment should be designed around the applicable requirements from the beginning.
What Information Should Be Provided to the Fire Pump Manufacturer?
To select and size a containerized fire pump efficiently, the manufacturer should receive as much project information as possible.
Useful information includes:
-
Required flow rate
-
Required pressure or head
-
System type
-
Building or facility application
-
Elevation difference
-
Water source information
-
Tank dimensions and minimum water level
-
Suction pipe information
-
Discharge pipe information
-
Required operating duration
-
Electrical voltage and frequency
-
Diesel engine requirements if applicable
-
Ambient temperature
-
Installation location
-
Container size limitations
-
Applicable standards
-
Certification or listing requirements
-
Project country and local requirements
With this information, a fire pump manufacturer can evaluate the hydraulic duty point and develop a complete package rather than selecting a pump based on incomplete information.
Final Checklist for Containerized Fire Pump Sizing
Before finalizing a containerized fire pump, confirm the following:
-
Required fire water flow has been established.
-
Required pressure has been calculated.
-
Elevation has been included.
-
Pipe friction losses have been calculated.
-
Fitting and equipment losses have been considered.
-
Water source conditions have been verified.
-
Pump type is appropriate for the application.
-
Pump performance curve has been reviewed.
-
Driver capacity has been verified.
-
Electrical requirements have been confirmed.
-
Diesel fuel requirements have been considered where applicable.
-
Container dimensions are sufficient.
-
Ventilation and exhaust requirements have been evaluated.
-
Maintenance access has been considered.
-
Environmental conditions have been evaluated.
-
Applicable standards and certification requirements have been confirmed.
-
The complete fire pump package has been reviewed as a system.
Conclusion
Correctly sizing a containerized fire pump requires a complete understanding of the fire protection system, not simply selecting a pump according to a required flow rate.
The design should begin with the required fire water demand and then account for pressure requirements, elevation, friction losses, water source conditions, pump performance, driver capacity, environmental conditions, and applicable standards.
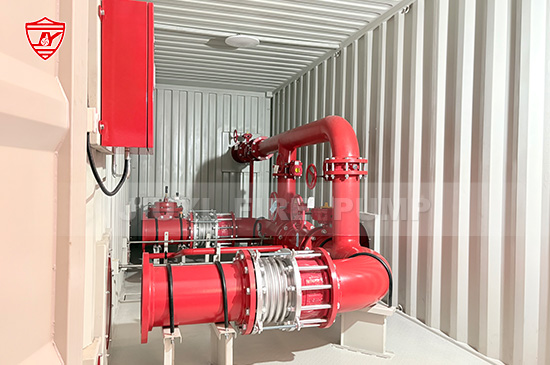
For containerized systems, the physical package is equally important. Pump, driver, controller, piping, valves, fuel system, ventilation, exhaust, monitoring equipment, and maintenance access must work together within the available enclosure.
A qualified fire pump manufacturer can help evaluate these requirements and develop a containerized fire pump package matched to the project's hydraulic and installation conditions.
By completing the hydraulic calculations and package requirements before equipment selection, project teams can reduce design changes, avoid undersized equipment, improve installation efficiency, and build a more reliable fire protection system.