.png)
.png)
.png)
How to Choose the Right Containerized Fire Pump for Your Project
Sep 03, 2026
Share:
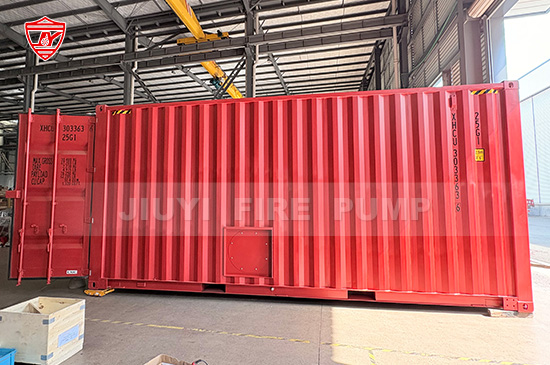
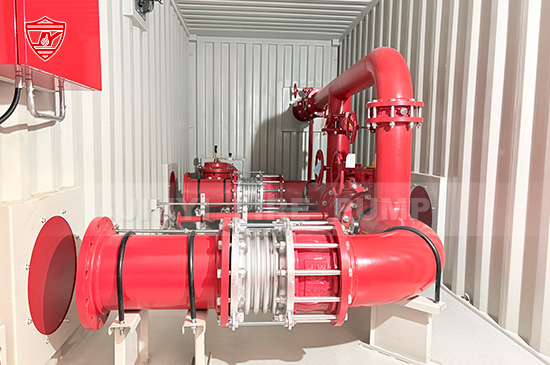
Choosing the right containerized fire pump is an important decision for projects where reliable fire protection is required but a conventional indoor pump room is difficult, expensive, or impractical to construct. A properly designed containerized fire pump system can integrate pumps, drivers, controllers, piping, fuel systems, ventilation, monitoring equipment, and other components into a factory-assembled enclosure.
However, not every containerized fire pump is suitable for every project. Flow requirements, pressure, pump configuration, power availability, environmental conditions, applicable standards, available space, installation requirements, and future maintenance all need to be considered before selecting a system.
For fire protection engineers, contractors, EPC companies, system integrators, and project owners, the following factors can help determine which containerized fire pump solution is appropriate.
1. Start With the Required Flow and Pressure
The first step is to determine the hydraulic requirements of the fire protection system.
A fire pump must provide sufficient flow at the pressure required by the sprinkler system, hydrants, hose stations, standpipes, or other fire protection equipment. The required duty point is normally determined through hydraulic calculations and the applicable fire protection design requirements.
For example, a project may require a fire pump capable of delivering 1,000 GPM at a specified pressure. Another project may require significantly higher flow because of the size of the protected facility or the type of hazard.
When selecting a containerized fire pump, do not select the pump based only on its maximum flow rating. The pump performance curve should be evaluated at the required operating point.
Key hydraulic parameters include:
-
Required flow rate
-
Required discharge pressure
-
Suction pressure
-
Static water level
-
Friction losses
-
Elevation difference
-
Required system pressure
-
Available water supply
-
Required flow range
The container itself should also have enough internal space for the selected pump, driver, piping, valves, controller, and auxiliary equipment.
2. Determine the Appropriate Fire Pump Type
The next consideration is the type of fire pump required by the application.
Containerized fire pump systems can be designed around different pump configurations depending on project requirements. Common options include electric fire pumps, diesel engine fire pumps, jockey pumps, horizontal split-case pumps, end-suction pumps, vertical turbine pumps, and other specialized configurations.
A horizontal fire pump can be suitable when the water source and suction arrangement allow the pump to operate correctly. A vertical turbine fire pump may be more appropriate when the water source is located below the pump installation level, such as a deep water tank or underground reservoir.
The pump type should therefore be selected based on both hydraulic performance and the physical characteristics of the water source.
For large-capacity systems, a split-case fire pump may provide a practical solution. For applications requiring a compact arrangement, an end-suction configuration may be considered where appropriate.
The correct selection depends on the complete fire protection design rather than the pump name alone.
3. Choose Between Electric and Diesel Drivers
The available power supply is another major factor.
Electric fire pumps can be an efficient solution when the project has a reliable electrical power source that meets the requirements of the fire protection system. The electrical infrastructure should be evaluated to ensure that the fire pump motor can start and operate as required.
Diesel engine fire pumps are commonly considered for projects where an independent mechanical power source is required or where electrical power reliability is a concern.
Some projects use a combination of electric and diesel-driven fire pumps to provide redundancy within the fire protection system.
A containerized system can accommodate the required driver arrangement while also incorporating supporting equipment such as:
-
Electric motors
-
Diesel engines
-
Fire pump controllers
-
Diesel engine controllers
-
Batteries and chargers
-
Fuel tanks
-
Exhaust systems
-
Ventilation systems
-
Cooling systems
The driver selection should be made together with the electrical, mechanical, and fire protection requirements of the project.
4. Consider Whether a Jockey Pump Is Required
A jockey pump is often an important component of a complete fire pump system.
Its primary purpose is to maintain system pressure and compensate for relatively small pressure losses without starting the main fire pump. This helps reduce unnecessary starting of the main electric or diesel fire pump.
When designing a containerized fire pump system, the jockey pump should be properly matched to the main fire pump and the system pressure requirements.
The jockey pump should not be selected simply according to the main pump's flow capacity. Its function, pressure setting, control logic, and relationship with the main fire pump need to be considered as part of the complete system.
Depending on the project, the containerized system may include a main electric fire pump, diesel fire pump, jockey pump, or a combination of these components.
5. Check Applicable Fire Protection Standards
Fire protection equipment must be selected according to the standards and approval requirements applicable to the project location.
Depending on the market and project specifications, requirements may involve standards and certifications such as UL Listed equipment, FM Approved equipment, NFPA requirements, or local fire protection regulations.
The exact requirements should be confirmed during the engineering stage.
For projects specifying UL Listed or FM Approved equipment, it is important to verify the certification status of the complete equipment and the individual components where required. Certification requirements may apply to pumps, motors, controllers, diesel engines, and other components.
Do not assume that a containerized fire pump is compliant simply because one component has a certification. The project specification should be reviewed carefully to determine what equipment and configurations require approval or listing.
6. Evaluate the Container Size and Internal Layout
One of the major advantages of a containerized fire pump system is that multiple components can be integrated into a single enclosure. However, the container must be large enough to accommodate the complete system while maintaining appropriate access for operation and maintenance.
The layout should consider:
-
Pump dimensions
-
Motor or engine dimensions
-
Controller location
-
Piping arrangement
-
Valve accessibility
-
Fuel tank location
-
Exhaust routing
-
Ventilation
-
Maintenance clearance
-
Electrical cable routing
-
Inspection access
-
Operator access
A compact layout can reduce transportation and installation requirements, but excessive space reduction may make maintenance difficult.
The goal is not simply to fit everything inside the container. The system should be arranged so that technicians can safely inspect, operate, repair, and replace critical components when necessary.
7. Consider Ventilation and Exhaust Requirements for Diesel Systems
Diesel-powered containerized fire pump systems require special attention to ventilation and exhaust design.
A diesel engine produces heat and exhaust gases during operation. The container must therefore be designed with an appropriate ventilation and exhaust arrangement.
Ventilation helps control the temperature inside the enclosure and provides the airflow required for engine operation. The exhaust system must safely discharge combustion gases away from the container and surrounding personnel.
Depending on the project, the system may require:
-
Ventilation fans
-
Air intake systems
-
Exhaust piping
-
Exhaust silencers
-
Temperature monitoring
-
Safety alarms
-
Engine cooling arrangements
The environmental conditions of the installation location should also be considered. A system designed for a moderate climate may require different ventilation or cooling provisions when installed in a high-temperature environment.
8. Check the Water Source and Suction Arrangement
The water source has a direct influence on fire pump selection.
Before selecting the pump, engineers should understand whether the system will draw water from a ground-level tank, elevated tank, underground reservoir, municipal water supply, or another source.
The suction conditions must be suitable for the selected pump configuration.
For vertical turbine fire pumps, the depth and configuration of the water source are particularly important. The pump bowl assembly, shaft arrangement, column length, discharge head, and water level all need to be considered.
For horizontal pumps, suction piping and available suction pressure must be evaluated carefully.
A containerized enclosure does not eliminate the need for proper hydraulic and suction design. The connection between the containerized pump package and the external water system remains a critical part of the installation.
9. Consider the Installation Environment
The location where the containerized fire pump will be installed can significantly affect the design.
Projects may be located in hot climates, cold climates, coastal areas, remote industrial facilities, mining sites, oil and gas facilities, warehouses, infrastructure projects, or temporary construction sites.
Environmental conditions may influence:
-
Container insulation
-
Ventilation
-
Heating
-
Cooling
-
Corrosion protection
-
Paint systems
-
Electrical protection
-
Fuel system design
-
Weatherproofing
For outdoor installation, the enclosure should be designed to protect the equipment from rain, dust, sunlight, and other environmental conditions appropriate to the project.
The containerized fire pump should therefore be designed around the actual installation environment rather than treated as a standard package for every application.
10. Think About Transportation and Site Installation
Transportation is another reason many projects choose containerized fire pump systems.
A factory-assembled unit can reduce the amount of field assembly required. However, transportation dimensions and weight must be considered from the beginning.
Project teams should check:
-
Container dimensions
-
Total shipping weight
-
Lifting points
-
Crane requirements
-
Truck access
-
Site access
-
Foundation requirements
-
External pipe connections
-
Electrical connections
For remote projects, minimizing complicated field installation can provide significant practical benefits.
The supplier should provide clear information about shipping dimensions, lifting arrangements, connection points, and installation requirements before production begins.
11. Evaluate Factory Assembly and Testing
Factory assembly and testing are important advantages of a professionally manufactured containerized fire pump system.
Instead of assembling every component at the project site, manufacturers can integrate and inspect the equipment in a controlled factory environment.
Depending on the system design and project requirements, factory inspection may include:
-
Pump performance testing
-
Motor testing
-
Diesel engine testing
-
Controller testing
-
Pressure testing
-
Piping inspection
-
Electrical inspection
-
Alarm and monitoring checks
-
System commissioning checks
For projects requiring specific certifications or customer inspection, testing procedures should be agreed upon before production.
Factory testing can also help identify installation or integration issues before the equipment reaches the project site.
12. Consider Maintenance and Long-Term Operation
A containerized fire pump should not be selected only according to its initial purchase price.
Fire protection equipment is expected to remain available when needed, potentially for many years. Maintenance accessibility and spare parts availability should therefore be considered during procurement.
Ask the manufacturer about:
-
Routine maintenance requirements
-
Recommended spare parts
-
Engine maintenance
-
Pump maintenance
-
Battery replacement
-
Controller servicing
-
Valve accessibility
-
Technical support
-
Documentation
-
Factory testing records
A well-designed container should provide sufficient working space around critical components.
Easy access to filters, batteries, controllers, valves, pumps, and engines can simplify maintenance and reduce downtime.
13. Work With the Manufacturer During the Design Stage
For customized containerized fire pump projects, early communication with the manufacturer can prevent many problems later.
The manufacturer should receive key project information such as:
-
Required flow and pressure
-
Fire pump configuration
-
Water source information
-
Power supply
-
Required certifications
-
Site climate
-
Installation location
-
Container dimensions
-
Fuel requirements
-
Control requirements
-
Piping connections
-
Transportation limitations
With this information, the manufacturer can develop a system configuration that matches the project's technical and installation requirements.
This approach is particularly important for large or customized projects where standard equipment may not meet the complete specification.
Conclusion: Select the Complete System, Not Just the Pump
Choosing the right containerized fire pump requires more than selecting a pump with a particular flow and pressure rating. The complete system must work together reliably, from the water source and pump to the driver, controller, piping, ventilation, fuel system, enclosure, and external connections.
The most important factors to review include hydraulic requirements, pump type, electric or diesel drive, jockey pump requirements, applicable certifications, container layout, environmental conditions, transportation, factory testing, and long-term maintenance.
For project owners, contractors, EPC companies, and fire protection engineers, working with an experienced fire pump manufacturer during the early design stage can help create a containerized fire pump system that is properly matched to the project's requirements.
A well-engineered containerized fire pump provides more than a compact equipment package. It can provide a coordinated fire protection solution designed for efficient installation, reliable operation, convenient maintenance, and the specific demands of the project.