.png)
.png)
.png)
How to Improve Fire Pump Efficiency
Sep 21, 2026
Share:
Fire pumps are critical components of fire protection systems. They must deliver the required flow and pressure when a fire occurs, often under demanding operating conditions. While reliability and fire protection performance are the primary priorities, fire pump efficiency also has a direct impact on energy consumption, operating costs, equipment life, and overall system performance.
Improving fire pump efficiency is not simply a matter of selecting a pump with a high efficiency rating. The complete fire pump system—including the pump, driver, piping, valves, controls, water supply, and operating conditions—must work together correctly. Poor pump selection, excessive pressure losses, improper maintenance, or operation far from the pump's best efficiency point can all reduce system efficiency.
For building owners, fire protection contractors, engineers, and facility managers, understanding the factors that influence fire pump efficiency can help create a more reliable and cost-effective fire protection system.
1. Select the Correct Fire Pump for the System
The first step in improving fire pump efficiency is selecting a pump that matches the actual requirements of the fire protection system.
A fire pump should be selected according to the required flow, pressure, water supply conditions, system elevation, friction losses, and other hydraulic requirements. Selecting a pump that is significantly oversized can result in inefficient operation and unnecessary energy consumption.
For example, if the required duty point is substantially lower than the pump's optimal operating range, the pump may operate away from its best efficiency point. This can increase energy consumption and may also create additional mechanical stress, vibration, recirculation, and wear.
The pump curve should therefore be carefully evaluated against the system demand curve before the equipment is selected. The goal is not simply to choose a pump with the highest possible capacity, but to select a pump that can reliably meet the required fire protection demand within an appropriate operating range.
2. Understand the Best Efficiency Point
The Best Efficiency Point, commonly known as the BEP, is one of the most important concepts when discussing pump efficiency.
A centrifugal fire pump has a specific operating point where it converts driver power into hydraulic output most efficiently. When a pump operates close to its BEP, hydraulic losses and mechanical stresses are generally minimized.
Operating too far to either side of the preferred operating range can reduce efficiency. It may also increase vibration, bearing loads, shaft deflection, internal recirculation, and other undesirable operating conditions.
During the design and selection process, engineers should compare the required system duty point with the manufacturer's certified pump performance curve. Selecting a pump whose performance characteristics closely match the system requirements can help improve efficiency throughout the expected operating range.
3. Reduce Unnecessary Pressure Losses
The efficiency of a fire pump is affected not only by the pump itself but also by the piping system connected to it.
Water flowing through pipes, fittings, valves, strainers, elbows, reducers, and other components experiences friction and pressure losses. If these losses are unnecessarily high, the fire pump must generate additional pressure to deliver the required flow at the system.
Proper hydraulic design can help reduce these losses.
Pipe sizing should be appropriate for the required flow rate, while unnecessary bends and restrictions should be minimized where practical. Valves and fittings should also be selected and installed correctly.
A well-designed suction arrangement is particularly important. Excessive suction losses can negatively affect pump performance and may increase the risk of cavitation.
Improving the hydraulic efficiency of the entire system can therefore reduce the amount of work required from the fire pump.
4. Maintain the Correct Suction Conditions
A fire pump needs an adequate and stable water supply to operate properly.
Insufficient suction pressure, restricted suction piping, blocked strainers, inappropriate pipe configuration, or excessive friction losses can affect pump performance. In severe cases, poor suction conditions can contribute to cavitation.
Cavitation occurs when local pressure in the pump falls sufficiently for vapor bubbles to form and subsequently collapse. This can cause noise, vibration, performance loss, and damage to internal components.
Proper suction pipe sizing, suitable water supply arrangements, correct valve positioning, and regular inspection can help maintain stable operating conditions.
For systems using water storage tanks, the tank arrangement and available water level should also be considered during system design and inspection.
5. Keep the Pump and Driver Properly Maintained
Regular maintenance is essential for maintaining fire pump efficiency.
A pump that is mechanically worn or improperly adjusted may require more input power to produce the same hydraulic output. Bearings, seals, couplings, shafts, impellers, and other components should therefore be inspected according to the equipment manufacturer's recommendations and applicable fire protection requirements.
The driver also plays an important role.
For electric motor-driven fire pumps, electrical connections, motor condition, voltage, current, insulation, and starting performance should be monitored as appropriate.
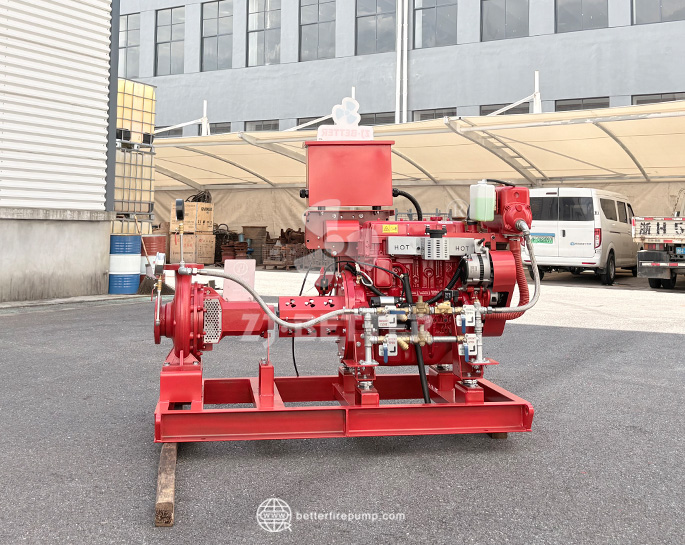
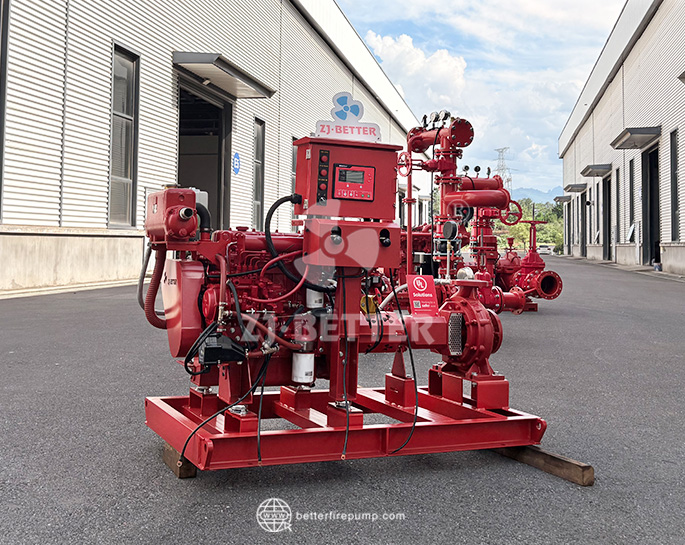
For diesel engine-driven fire pumps, engine condition, fuel quality, batteries, cooling systems, lubrication, exhaust systems, and starting equipment require regular attention.
A well-maintained driver can deliver the required mechanical power more reliably and efficiently.
6. Perform Regular Fire Pump Testing
Testing provides valuable information about the actual condition and performance of a fire pump.
A fire pump test can help identify changes in flow, pressure, starting performance, vibration, or other operating characteristics. Comparing current test results with previous results can also help identify gradual performance deterioration.
During testing, the pump should be evaluated at appropriate flow conditions according to the applicable requirements and testing procedures.
If test results show that the pump is no longer performing as expected, the cause should be investigated rather than simply adjusting the system to compensate.
Regular testing can therefore serve as both a fire protection requirement and an important performance-monitoring tool.
7. Keep Fire Pump Components Properly Aligned
Mechanical alignment is another factor that can influence fire pump efficiency and equipment life.
Pump and driver shafts must be properly aligned according to the manufacturer's requirements. Misalignment can increase vibration and mechanical loads and may contribute to premature wear of couplings, bearings, and other components.
Coupling condition should also be inspected as part of routine maintenance.
Correct installation and alignment help ensure that the power produced by the driver is transferred efficiently to the pump without unnecessary mechanical losses.
8. Keep Impellers and Internal Components in Good Condition
The impeller is one of the most important hydraulic components of a centrifugal fire pump.
Over time, corrosion, erosion, deposits, or mechanical damage can affect the condition of the impeller and other internal surfaces. Changes in hydraulic clearances can also affect pump performance.
If a pump shows a noticeable reduction in performance, the cause should be investigated. In some cases, internal inspection may be necessary to determine whether wear or damage is affecting the hydraulic performance.
Using suitable materials and manufacturing processes during pump production can also contribute to long-term performance and reliability.
9. Select an Appropriate Fire Pump Driver
The driver must be capable of supplying the power required by the fire pump under the complete operating range.
Electric motors and diesel engines have different operating characteristics, and the selection should reflect the requirements of the application.
For electric fire pumps, the electrical supply should be capable of supporting the required motor performance. Voltage conditions, cable sizing, control equipment, and starting requirements should all be considered as part of the system design.
For diesel fire pumps, engine output, cooling, ventilation, fuel supply, exhaust arrangements, and environmental conditions are important considerations.
Correct driver selection ensures that the pump can operate reliably without unnecessary power limitations or inefficient operation.
10. Avoid Oversizing the Fire Pump
Oversizing is a common consideration when discussing fire pump system efficiency.
It is understandable that project designers may want to provide additional capacity, but excessive oversizing can create undesirable operating conditions.
A pump that produces substantially more flow or pressure than the system requires may operate away from its optimal range. Excessive pressure can also create additional system losses and may require pressure management within the fire protection system.
Fire pumps should therefore be selected based on the actual hydraulic requirements and applicable fire protection design criteria rather than simply choosing the largest available model.
11. Keep Valves and Accessories in Proper Condition
Valves and accessories can have a significant effect on system hydraulic performance.
Partially closed valves, damaged components, clogged strainers, or inappropriate installation can create additional pressure losses. These conditions may force the pump to work harder to achieve the required system performance.
Routine inspection should verify that relevant valves are in their required operating positions and that components are free from unnecessary restrictions.
A fire pump system should be viewed as an integrated system rather than as an isolated pump.
12. Consider the Entire Fire Pump System
Improving fire pump efficiency requires a system-level approach.
The pump, driver, controller, piping, valves, water source, storage tank, pressure conditions, and downstream fire protection equipment all interact with one another.
For example, a highly efficient pump cannot compensate for an unnecessarily restrictive piping system. Similarly, an appropriately selected pump may not perform correctly if the suction conditions are inadequate.
System designers and facility operators should therefore evaluate hydraulic performance from the water source through the pump and into the fire protection network.
This approach can reveal opportunities to reduce unnecessary losses while maintaining the required fire protection performance.
13. Use Factory Testing to Verify Pump Performance
Factory testing is an important part of fire pump quality assurance.
Before delivery, manufacturers can test pumps under controlled conditions to verify flow, pressure, speed, power, and other performance characteristics.
A properly equipped fire pump manufacturer can evaluate pump performance across multiple operating points and compare test results with the specified performance requirements.
For customers, factory testing provides valuable performance information before equipment reaches the project site.
For manufacturers, advanced testing equipment and controlled production processes also help identify potential issues before shipment.
14. Monitor Changes in Pump Performance
Efficiency should not be considered only during initial pump selection.
Fire pump performance can change over time because of wear, changes in water conditions, maintenance issues, or modifications to the fire protection system.
Maintaining historical test data makes it easier to identify trends.
For example, if the measured flow and pressure gradually decline over multiple tests, this may indicate a developing mechanical or hydraulic issue. Early investigation can help prevent more serious performance deterioration.
Performance monitoring is therefore an important part of maintaining long-term fire pump efficiency.
15. Balance Efficiency With Fire Protection Reliability
The objective of improving fire pump efficiency is not to reduce pump capacity at the expense of fire safety.
A fire pump is first and foremost a life-safety component. Its primary function is to provide the required water flow and pressure when the fire protection system needs it.
Energy efficiency, operating cost, and equipment life should therefore be considered together with the applicable fire protection requirements.
A properly selected and maintained fire pump can provide reliable fire protection while minimizing unnecessary hydraulic and mechanical losses.
Conclusion
Improving fire pump efficiency requires more than choosing an efficient pump. It involves correct hydraulic design, proper pump selection, appropriate driver sizing, good suction conditions, regular maintenance, accurate testing, and continuous performance monitoring.
The most important factors include selecting a pump near the appropriate operating range, reducing unnecessary piping losses, maintaining pump and driver components, preventing suction problems, and verifying performance through regular testing.
For fire pump manufacturers, efficiency begins during engineering and production. Accurate hydraulic design, controlled manufacturing processes, appropriate materials, precision machining, professional assembly, and comprehensive factory testing all contribute to reliable pump performance.
For building owners, contractors, engineers, and fire protection professionals, taking a system-level approach can help improve operating efficiency without compromising the reliability of the fire protection system.
Next: